Welding · LPG cylinder production line
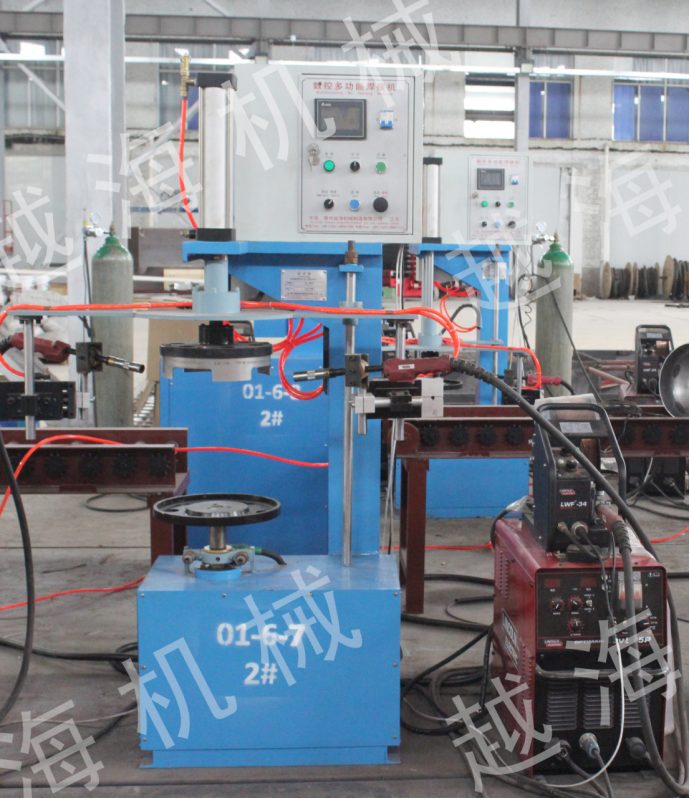
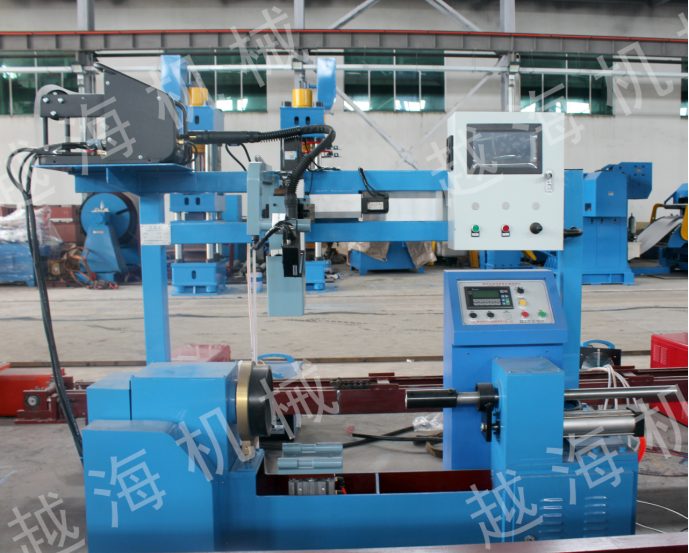
Both sides of the circumferential seam arc at the same time, balancing heat input so ovality change stays small and no re-rounding pass is needed.
The torch follows the joint in real time, so fit-up variation in incoming parts does not turn into weld deviation.
Each cylinder type and plate thickness has a stored program; a size change is a recipe call, not a manual setup.
Standard machine data below. Non-standard sizes can be tooled to your cylinder drawings.
| Twin-torch circumferential | — |
|---|---|
| Air pressure | 0.6–0.8 MPa |
| Cycle time | 12–16 s/pc |
| Sheet thickness | 2.0 – 6.0 mm |
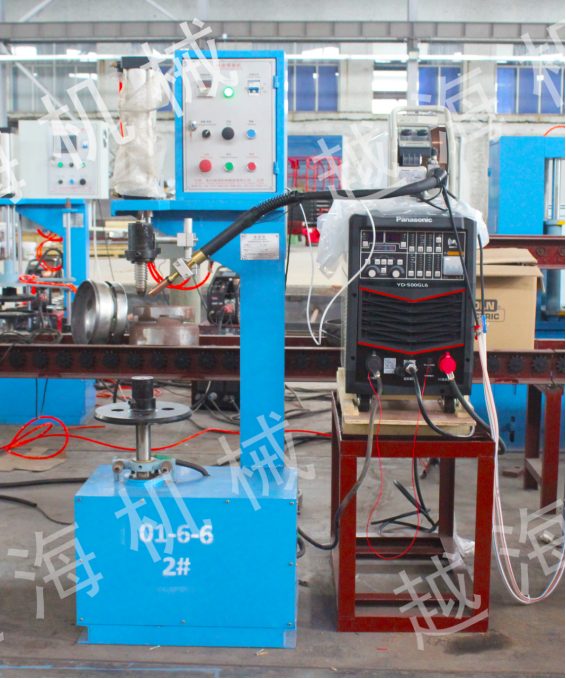
| Welding process | MAG / submerged arc (per process) |
| Seam acceptance | ≥ 99.5% (RT sampling) |
| Power supply | AC 380 V / 50 Hz, 3-phase + N + PE (customized to destination) |
| Protection | Control cabinet IP54, actuators IP65 |
| Lead time | 60 – 90 days after contract effectiveness |
The more specific your information, the more accurate the quote. Ideally include: cylinder size (1 / 5 / 12.5 / 15 / 25 / 50 kg), sheet thickness, target daily output, existing process and available floor area.